The Chart Every Machinist Keeps At The Bench
Standard, Metric & Pipe — All In One Place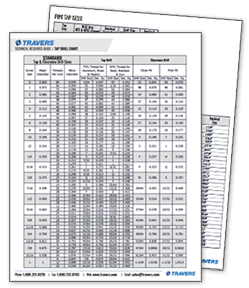
Choosing the wrong tap drill costs you a broken tap, a stripped hole, or a scrapped part. This guide gives you the exact drill size for standard (UNC/UNF), metric, and pipe threads — at both 75% and 50% thread engagement — so you get it right the first time.
You'll get:
- Standard tap & clearance drill sizes (UNC/UNF)
- Metric tap drill sizes by pitch
- NPT & NPS pipe tap drill sizes
- Plug tap sizes and major/minor diameters
Standard tap drill chart (UNC / UNF, inch)
Use the 75% thread drill for aluminum, brass, and plastics, and the 50% thread drill for steel, stainless, and iron. Clearance drills are for through-holes the screw passes through.
| Thread | TPI | Tap drill 75% (Al, brass, plastic) |
Tap drill 50% (steel, stainless) |
Clearance close fit |
Clearance free fit |
|---|---|---|---|---|---|
| #4-40 | 40 | #43 (.089) | #41 (.096) | #32 (.116) | #30 (.129) |
| #6-32 | 32 | #36 (.107) | #32 (.116) | #27 (.144) | #25 (.150) |
| #8-32 | 32 | #29 (.136) | #27 (.144) | #18 (.170) | #16 (.177) |
| #10-24 | 24 | #22 (.157) | #20 (.161) | #9 (.196) | #7 (.201) |
| #10-32 | 32 | #21 (.159) | #18 (.170) | #9 (.196) | #7 (.201) |
| 1/4"-20 | 20 | #7 (.201) | 7/32" (.219) | F (.257) | H (.266) |
| 1/4"-28 | 28 | #3 (.213) | #1 (.228) | F (.257) | H (.266) |
| 5/16"-18 | 18 | F (.257) | J (.277) | P (.323) | Q (.332) |
| 5/16"-24 | 24 | I (.272) | 9/32" (.281) | P (.323) | Q (.332) |
| 3/8"-16 | 16 | 5/16" (.313) | Q (.332) | W (.386) | X (.397) |
| 3/8"-24 | 24 | Q (.332) | S (.348) | W (.386) | X (.397) |
| 7/16"-14 | 14 | U (.368) | 25/64" (.391) | 29/64" (.453) | 15/32" (.469) |
| 1/2"-13 | 13 | 27/64" (.422) | 29/64" (.453) | 33/64" (.516) | 17/32" (.531) |
| 1/2"-20 | 20 | 29/64" (.453) | 15/32" (.469) | 33/64" (.516) | 17/32" (.531) |
| 5/8"-11 | 11 | 17/32" (.531) | 9/16" (.563) | 41/64" (.641) | 21/32" (.656) |
| 3/4"-10 | 10 | 21/32" (.656) | 11/16" (.688) | 49/64" (.766) | 25/32" (.781) |
Metric tap drill chart (mm)
Drill sizes for coarse-pitch metric threads. The pitch drives the drill size — always match both (e.g. M8×1.25).
| Thread × pitch | Tap drill 75% (mm) | Tap drill 50% (mm) |
|---|---|---|
| M3 × 0.5 | 2.50 | 2.70 |
| M4 × 0.7 | 3.30 | 3.50 |
| M5 × 0.8 | 4.20 | 4.50 |
| M6 × 1.0 | 5.00 | 5.40 |
| M8 × 1.25 | 6.80 | 7.20 |
| M10 × 1.5 | 8.50 | 9.00 |
| M12 × 1.75 | 10.30 | 10.90 |
| M14 × 2.0 | 12.10 | 12.70 |
| M16 × 2.0 | 14.00 | 14.75 |
| M20 × 2.0 | 18.00 | 18.50 |
Pipe tap drill chart (NPT / NPS)
Tapered pipe threads (NPT / NPTF) seal by wedging; straight pipe threads (NPS) do not.
| Tap size | Drill — NPT / NPTF (taper) | Drill — NPS (straight) |
|---|---|---|
| 1/8"-27 | R (.339) | S (.348) |
| 1/4"-18 | 7/16" (.4375) | 29/64" (.4531) |
| 3/8"-18 | 37/64" (.5781) | 19/32" (.5938) |
| 1/2"-14 | 23/32" (.7188) | 47/64" (.7344) |
| 3/4"-14 | 59/64" (.9219) | 15/16" (.9375) |
| 1"-11.5 | 1-5/32" (1.1562) | 1-3/16" (1.1875) |
| 1-1/4"-11.5 | 1-1/2" (1.5000) | 1-33/64" (1.5156) |
| 1-1/2"-11.5 | 1-47/64" (1.7344) | 1-3/4" (1.7500) |
| 2"-11.5 | 2-7/32" (2.2188) | 2-7/32" (2.2188) |
Need every size on one FREE OF COST printable sheet?
Download the complete Tap & Drill Chart PDF — all standard, metric, plug tap and pipe sizes.
How to use a tap drill chart
A tap drill chart tells you the hole size to drill before cutting internal threads with a tap. Pick the right size and the thread is strong and the tap runs freely; too small and you spike tapping torque and risk snapping the tap; too large and the threads lose holding strength.
75% vs 50% thread engagement
Most shop work targets about a 75% thread — the best balance of strength and ease of tapping. In tougher materials like steel and stainless, dropping to roughly 50% thread (a slightly larger drill) cuts tapping torque and tap breakage with little loss of holding power.
Major vs minor diameter
The major diameter is the distance across the outer crests of the thread; the minor diameter is across the inner roots. The tap drill produces a hole close to the minor diameter so the tap can cut clean threads.
Do you drill for a die too?
No. A tap cuts internal threads and needs a drilled hole first. A die cuts external threads onto a rod or bolt and needs no drill — so a "tap and die drill chart" really only applies to the tapping side.
Shop the tools for the job
Frequently asked questions
What size drill do I use for a 1/4"-20 tap?
Use a #7 drill (0.201") for a 1/4"-20 UNC thread at 75% thread engagement.
What drill size is used for an M8 tap?
An M8×1.25 thread uses a 6.8 mm drill. For the fine-pitch M8×1.0, use 7.0 mm.
What thread engagement should a tap drill give?
About 75% for general work; roughly 50% in steel and stainless to lower tapping torque.
Do I need a drill size for a die?
No. Dies cut external threads and need no drilled hole — only taps require a tap drill.